September 2, 2026
What Battery Enclosure Fabrication Can Teach About Heavy Duty Trolley Design
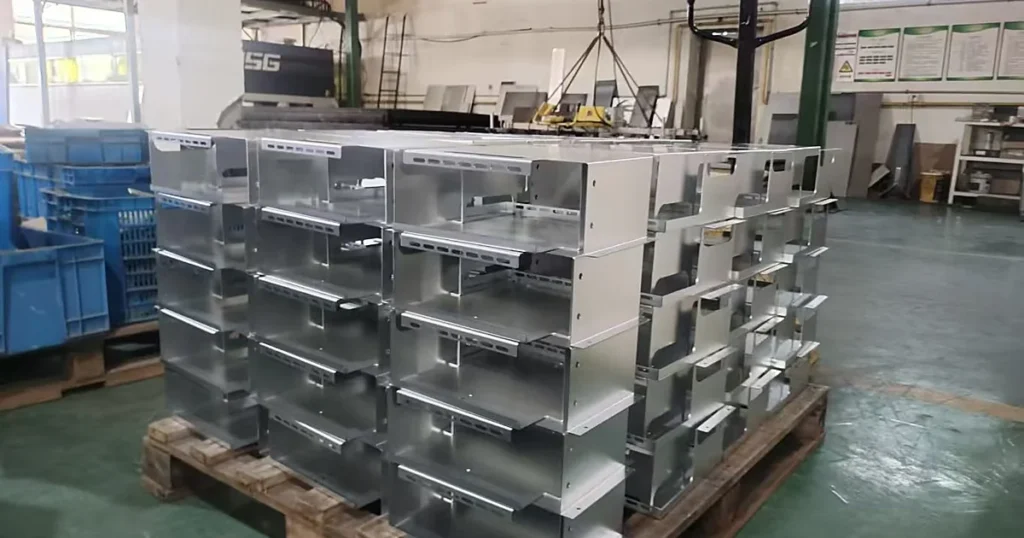
Some of the most demanding sheet metal work being specified today is for battery enclosures, energy storage racks and precision electronic housings. Those jobs are useful to anyone specifying a heavy-duty trolley, because the disciplines that make them succeed are exactly the disciplines that separate a trolley that lasts from one that does not: dimensional control, bend consistency, weld distortion control, coating coverage, assembly fit and inspection records.
What enclosure work and trolley work share
It is easy to assume a battery enclosure is a harder job than a trolley because it is more tightly toleranced. In most respects the underlying requirements are the same:
- Hole accuracy. An enclosure needs holes that line up with a busbar or a cell module. A trolley needs caster bolt holes that line up with a frame, and shelf holes that line up with a fixture. The consequence of error is identical: parts that will not assemble without force.
- Formed panel consistency. An enclosure lid must sit flat on a gasket. A trolley shelf must sit flat in a frame. Both depend on bend angle repeatability, not on one skilled operator having a good day.
- Weld distortion control. An enclosure that is out of square will not seal. A trolley that is out of square will not track straight. Same problem, different symptom.
- Corrosion protection. Both may work in humid, outdoor or chemically aggressive environments, and both fail first at edges, welds and crevices.
- Assembly fit. Both are assembled with other people’s components — fasteners, slides, latches, electronics — and interface dimensions have to be held.
- Documentation. Both benefit from inspection records when a buyer has to approve a first article or audit a repeat order.
Where trolley design is genuinely different
The important difference is that a trolley is dynamic. An enclosure sits still; a trolley moves, turns, brakes, crosses thresholds, and carries a load that changes from trip to trip. That adds four disciplines that enclosure work does not teach:
- Wheel and caster selection. Nothing in a stationary enclosure prepares you for specifying tread material, diameter, bearing type and brake layout against a real floor and a real route.
- Load distribution and dynamics. Static load ratings do not capture shock loading, uneven distribution, or the lateral forces in a turn.
- Handle ergonomics. Pushing force, handle height, grip diameter and reach decide whether the trolley is used correctly every day.
- Packing for bulky assemblies. An enclosure ships in a crate; a trolley is awkward, hollow, and easy to damage in a container. Packing is part of the design.
So the manufacturing discipline transfers in full; the application engineering does not. A supplier who is good at enclosures is not automatically good at trolleys, and the reverse is equally true.
The specification habits worth copying
Four practices from high-specification enclosure work are worth carrying into any heavy trolley enquiry:
1. Mark the critical dimensions
Not every dimension can be critical; if they all are, none are. Identify the interfaces that must be held — caster bolt pattern, shelf fixing centres, handle mounting, overall footprint — and say so on the drawing.
2. Freeze the drawing before the run
Version the file. A drawing that is changed verbally mid-run produces a mixed batch, and the mismatch usually surfaces at assembly or at the customer’s site.
3. Ask for a first-article check
One assembled unit, checked against the drawing before the rest are built. On a trolley this should include a trial fit of the casters, a flatness check, and operation of any drawer, door or folding mechanism.
4. Decide what gets inspected and documented
Dimensional checks, weld inspection, coating thickness, or simply a visual standard. Agree it before production so the cost is in the quote rather than in a dispute afterwards.
Material and thickness choices, compared
Enclosure work often runs in thinner, tightly toleranced material; trolley work spreads across a wider band because different parts do different jobs:
- 0.8–1.5 mm — drawer bodies, covers, bin fronts, light panels.
- 1.5–3.0 mm — shelves, decks, caster plates, brackets, guards.
- 3.0 mm and above — heavy caster mounts, tow bar brackets, forklift pockets.
- Tube — commonly 20–50 mm outside diameter with 1.2–3.0 mm wall, chosen by span and duty rather than by habit.
The discipline worth copying from enclosure work is stating the grade explicitly. “Steel” is not a specification; neither is “stainless”. Grade, thickness and finish should all appear on the drawing.
When a heavy-duty trolley really is heavy duty
“Heavy duty” is used so loosely that it has almost no meaning. These are the conditions that genuinely change the design, and all of them should be stated in an enquiry:
- Payload and distribution — including worst case, and whether loads are placed by hand or by machine.
- Shock loading — dropped loads, thresholds, dock plates.
- Duty cycle — occasional moves versus continuous shift work, which drives bearing and wheel choice.
- Route and floor — distance, surface, slope and transitions.
- Environment — humidity, washdown, chemicals, outdoor storage.
- Expected life and replacement cycle — which determines whether a fixture is worth building.
Frequently asked questions
Do I need the same tolerances as an enclosure?
Rarely, and asking for them everywhere will increase cost for no benefit. Identify the interfaces that need accuracy and specify those; leave the rest at normal fabrication tolerance.
What makes a trolley “heavy duty” in practice?
Not the label — the combination of payload, shock loading, duty cycle and route. A 300 kg trolley used continuously on a rough floor is a harder design problem than a 1000 kg trolley moved twice a day on smooth concrete.
Can you inspect to a documented standard?
Yes, if it is agreed before quoting. State which dimensions are checked, what is recorded, and whether a first-article report is required.
Is a prototype worth the cost?
For a new design that will repeat, almost always. One prototype finds the fit, ergonomics and packing issues that a drawing cannot — and it is far cheaper than discovering them across a full production run.
RFQ details
- Critical dimensions and assembly interfaces, marked on the drawing.
- Load magnitude, distribution and direction, plus shock loading expectations.
- Route, floor condition, duty cycle and expected service life.
- Cut, bend, weld and finish requirements, with material grades stated.
- Inspection documents needed for internal approval.
- Repeat-order control: colour reference, wheel model, caster layout and packing method.
Good trolley work borrows its discipline from the most demanding jobs in the shop and applies it to something that has to roll. Send your drawing and service conditions, or start from the build-to-print page if you already have drawings ready.
Related pages: manufacturing processes, quality control, and trolley products.
Have a Similar Trolley Project? Send It for Review
Send your trolley type, load capacity, size, wheel requirement, quantity, and drawings or reference photos. Our team will review the structure and reply within 24 hours on business days.
Urgent project? Email gao@doingmetal.com or WhatsApp +86 18158549983.