October 9, 2026
Wet Paint vs Powder Coating: When a Part Is Outside Our Scope
The short answer first
We are a powder coating shop. Every trolley and sheet metal part we ship leaves Ningbo with dry powder applied and cured in our own line. We do not run a wet paint booth, we do not spray 2K polyurethane or acrylic, and we do not handle solvent-based paint. If your drawing calls for painted parts, you need a different supplier for that operation, and it is better to know that in the first email than in the third week.
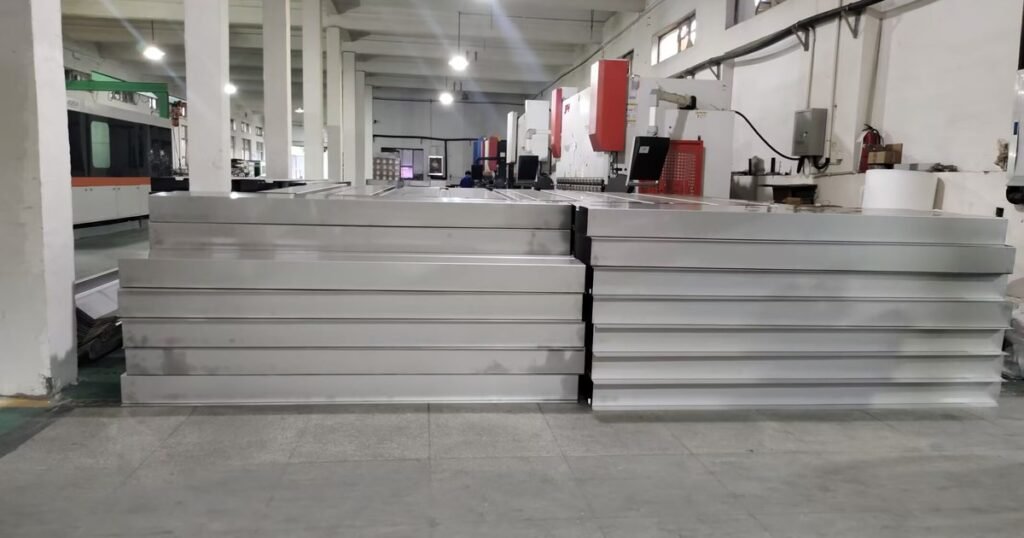
That sounds like a limitation, so here is the rest of it: we are unusually good at the operations that sit either side of painting. Laser cutting, CNC bending, tube work, frame welding, powder coating, assembly and inspection are all in-house, which means the parts that arrive at a paint booth are already geometrically correct and properly prepared. Most paint problems are preparation problems, and preparation is exactly what a fabrication shop controls.
Powder coating versus wet paint, honestly
Both are legitimate. They are not competitors, and a good buyer specifies one for a reason rather than by habit.
- Powder coating is the default for indoor industrial work. It is dry, it carries no solvent, it is thick in a way wet film is not, and it takes a chip without showing bare metal underneath the same way. It is also easy to repeat: the same RAL reference on the same pretreatment gives a visually consistent result across a repeat order, which matters more to a brand than most buyers expect.
- Wet paint — 2K polyurethane, acrylic, and similar — gives a wider colour space, different texture options, and often a thinner film. It is the right answer for a product with a painted appearance requirement rather than a durability requirement: a machine housing, a medical device cover, an enclosure that has to match a brand’s existing product colour.
- Hot-dip galvanizing is not paint at all and is a different decision again — it is the outdoor and corrosion-led choice.
If you need a painted appearance, specify it as a separate operation and expect to pay for two suppliers and one extra transport leg. That is a normal arrangement, not a problem. We are happy to supply the fabricated, cleaned and prepared parts to your paint house with a documented prep specification.
What we do in-house, and what that means for your part
| Operation | In-house? | What it means for you |
|---|---|---|
| Laser cutting (fibre, sheet and plate) | Yes | Flat parts cut from your DXF or STEP, no subcontract, no re-handling damage |
| Laser cutting + turret punching | Yes | If your package combines a profile and a perforated zone, both happen in one setup |
| CNC press-brake bending | Yes | Formed features with consistent angles; boxes, trays, returns, flanges |
| Tube laser and tube bending | Yes | Frames, handles, tubular structure to a welded assembly |
| MIG / TIG welding | Yes | Frames and weldments, jigged so the part comes out square |
| Powder coating | Yes | Pretreatment, powder, cure; RAL or Pantone reference matched to a defined limit |
| Assembly and packing | Yes | Casters fitted, fasteners torqued, export packing, loading plan |
| Wet paint / 2K PU / solvent spray | No | Route to your own paint house; we supply prepared parts and a prep spec |
| Casting, forging, machining | No | Buy machined parts in separately, or we buy them for you |
| Electronics, wiring, castor assembly by us | No | We fit customer-specified castors; we do not supply motors or electronics |
How powder coating fails, and how that is prevented
Most coating complaints trace back to one of four things, and all four are decided before the part ever enters the booth.
1. Coating over oil and cutting fluid
Steel is cut with lubricant. If it goes into a pretreatment line still carrying oil, the coating adheres to the oil film rather than to the steel, and the defect appears weeks later as blistering or peeling. Every part goes through degreasing and a rinse check before powder is applied.
2. Coating over rust
Mill scale and light surface rust are removed in pretreatment. Heavy corrosion is not a coating problem — it is a material problem, and it is cheaper to change the material specification than to fight it.
3. Welds and edges
A weld bead is a different surface to the surrounding sheet. Where a weld will be visible and handled, tell us whether it is ground, blended, or acceptable as-raised. Powder on a ground weld and powder on a raw weld will not match in gloss, and pretending otherwise is how “the finish looks different” arguments start.
4. The classic: coating a part that is still a sub-assembly
A trolley is assembled, then coated, then assembled again. If a part is coated while it is already welded into a frame and there are masked areas, the masked area will show as a difference in colour and texture. Send us the coating boundaries as a separate layer or a marked-up drawing, not as a verbal instruction.
What to write in the RFQ so we quote the right thing
- Colour reference by standard — RAL or Pantone — and whether a visible match to an existing product is required.
- Coating thickness expectation, if you have one. Typically we specify a normal decorative range for indoor trolley work.
- Gloss level: matt, satin or gloss.
- Which surfaces are visible in service, and which are acceptable as-raised or as-welded.
- Any masking: threads, mounting faces, contact pads, labels, or areas that must stay bare.
- The service environment: indoor, washdown, outdoor, marine, food-adjacent, or a container that will sit unopened for months.
- Whether repeat orders will follow, and whether you need a colour reference panel or a first-article coated sample approved before batch.
If a painted part is genuinely what your project needs, say so in your first message and give the paint house you intend to use. We will tell you honestly whether the fabrication package is worth quoting from us, and if the answer is no, we will say that instead of quoting you a part that will not pass your own coating check.
Frequently asked questions
Can you paint parts if I supply the paint?
No. We have no booth, no spray equipment and no ventilated painting area. Supplying your own paint does not change that.
Can you ship fabricated parts to my paint house?
Yes. We supply parts with a documented pretreatment state and a packing specification that keeps flanges and machined faces protected, and we can ship to your paint house or hold for your collection.
Can you match a colour to a sample we already have?
Send a physical sample, not a photograph. A photograph cannot tell you the gloss level, and gloss is usually what makes a coated part look wrong against an existing product.
Do you coat stainless steel?
We do not powder coat stainless as a standard. Stainless is normally supplied in a 2B or ground finish, and if appearance matters it is better to discuss brushed or polished grain direction before production than to try and mask it afterwards. Passivation and electro-polishing are also different operations from coating — tell us which one your drawing means.
Do you cut and form parts that will be painted by someone else?
That is a large part of what we do. Send the paint house drawing and we will supply parts that are flat, clean, deburred and correctly prepared for it.
Not sure which process your part actually needs? Send the drawing and the service environment and we will tell you which finishes we can deliver and which we cannot — including when the honest answer is that a different supplier is better for your part. Our finish guidance covers the trade-offs between powder coating, galvanizing and stainless in more detail in the surface treatment guide.
Related pages: Industrial trolley surface treatment and Quality control and inspection.
Have a Similar Trolley Project? Send It for Review
Send your trolley type, load capacity, size, wheel requirement, quantity, and drawings or reference photos. Our team will review the structure and reply within 24 hours on business days.
Urgent project? Email gao@doingmetal.com or WhatsApp +86 18158549983.