September 2, 2026
Welding Distortion Control for Heavy Duty Trolley Frames
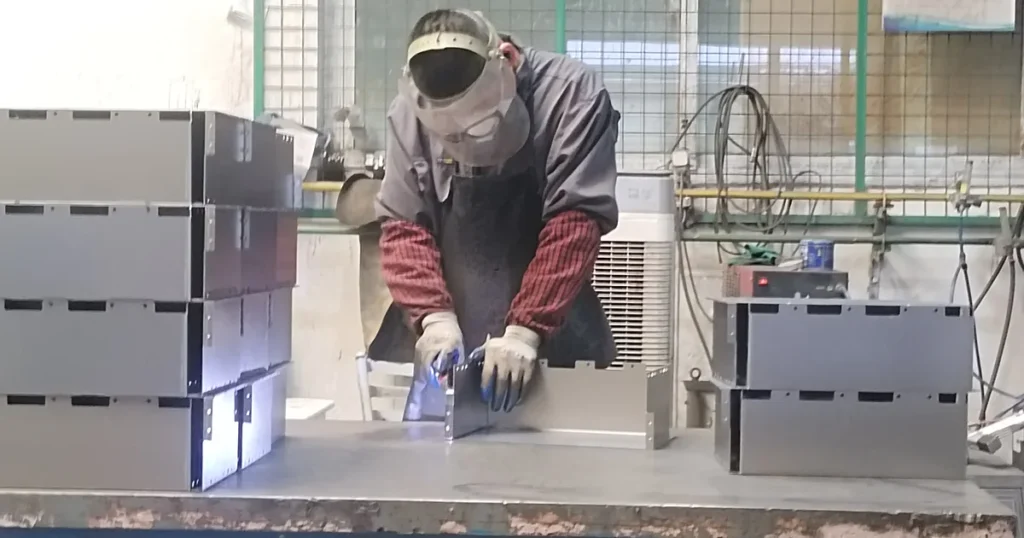
Welding decides whether a trolley runs straight. A trolley frame looks like a simple assembly of tube and plate, but every weld puts heat into the structure, and heat moves metal. The consequences show up as a deck that is not flat, caster plates that are not coplanar, a frame that is not square, or a handle that sits visibly off-centre. None of these affect the load rating printed on the drawing — and all of them affect whether the trolley is pleasant to use for the next ten years.
What distortion actually costs
Distortion is not a cosmetic issue. On a trolley it produces measurable functional problems:
- Caster plates out of plane. If the four mounting faces are not coplanar, one wheel carries less load and the trolley pulls to one side. Operators compensate by pushing harder, which is when complaints start.
- Frame out of square. Diagonal mismatch makes the trolley track crooked and makes shelves, drawers and doors bind.
- Deck not flat. Loads rock, cartons slide, and point loads concentrate where they were never intended.
- Handle asymmetry. Immediately visible, and usually the first thing a customer notices on delivery.
- Wheel alignment. Even small angular errors at the caster mount translate into scrub and rapid tread wear over thousands of metres.
Where distortion comes from
Three mechanisms do most of the damage, and all three are manageable:
- Uneven heat input. Welding one side of a joint before the other pulls the assembly towards the weld. This is the dominant cause.
- Thin sections and long spans. Thin tube and wide sheet assemblies have little inherent stiffness to resist the shrinkage forces. A 1.5 mm shelf distorts far more readily than a 6 mm plate.
- Restraint that is either absent or excessive. Unrestrained parts move freely; over-restrained parts build stress that releases later, sometimes after coating.
Fixture control: the real answer for repeat orders
For a one-off prototype, a skilled welder can correct as they go. For a repeat order of twenty, fifty or five hundred units, that is not a method — it is a source of variation. Fixtures are what make unit fifty match unit one.
A well-designed trolley fixture holds:
- Caster plates in a fixed, coplanar relationship — usually the most important dimension on the whole trolley.
- Side rails and uprights at the correct spacing and square to the base.
- Handles symmetrically, so they do not need individual adjustment.
- Shelves and mesh panels at the correct pitch, so assembled units are interchangeable.
- Foldable structures in the open position, so the mechanism is aligned the same way every time.
Fixtures cost money and take time to build, which is why they only make sense when a design will repeat. If you expect follow-on orders, say so at the quotation stage — it changes how the job is planned and it is far cheaper to do right the first time.
Welding sequence and heat control
Sequence is free; it costs nothing but planning.
- Balance the welds. Weld opposite sides in alternation rather than completing one side and moving on.
- Stitch and skip. A long continuous weld puts far more heat into a joint than a series of short stitches. Where full strength is not required, stitch welding reduces distortion and often looks better.
- Weld from the centre outwards on long joints, so shrinkage is distributed.
- Tack fully before welding. A properly tacked assembly holds its geometry; a poorly tacked one moves before the first real weld is laid down.
- Control heat input. Correct settings for the material thickness — too much heat on thin tube is the fastest way to a warped frame.
Visible welds versus structural welds
These are different jobs and should be specified differently:
- Structural welds — caster mounts, load-bearing joints, handle roots — are specified for penetration and strength. Appearance is secondary, though they must be clean before coating.
- Visible welds — on customer-facing trolleys, retail cages, library trucks and studio carts — are specified for appearance: even bead, minimal spatter, and a consistent finishing method.
- Grinding and dressing. Decide what gets ground, what gets dressed, and what is left as-welded. This is a cost item and a quality expectation; it should be stated rather than assumed.
Inspection points that matter on a trolley
A checklist that catches the problems while they can still be fixed:
- Frame squareness — diagonal measurement against the drawing.
- Caster plate flatness and hole position — checked before coating, not after.
- Wheel alignment — a trial fit on a flat surface is the most honest test.
- Weld bead consistency and absence of visible defects on cosmetic welds.
- Handle rigidity and side rail alignment.
- Sharp-edge removal before powder coating — a sharp edge will not hold coating, and coating failure starts there.
- Drawer, door and fold mechanism operation on a trial assembly, before the run starts.
Design choices that reduce distortion
Some of this can be solved on the drawing, before any heat is applied:
- Symmetric weld layouts where possible, so shrinkage balances.
- Fewer, longer parts instead of many short pieces joined end to end.
- Formed sections rather than welded-up box sections, where the geometry allows — a folded section arrives straight and needs fewer welds.
- Realistic tolerances on non-critical dimensions, so effort goes where it matters.
- Fixturing features designed into the parts, so the assembly can be held repeatably.
Frequently asked questions
Can a warped frame be straightened after welding?
Sometimes, by controlled mechanical correction or localised reheating, but it adds cost and can leave residual stress. Prevention through sequence and fixtures is cheaper and more reliable.
Are fixtures worth it for a small order?
Usually not for a single unit. For any order likely to repeat, yes — the fixture is what makes the second batch match the first.
Why does my trolley pull to one side?
Most often because the caster mounting faces are not coplanar, or the wheel alignment is off. Both are fixturing and inspection issues, and both should be checked before coating.
Should all welds be ground smooth?
Not necessarily, and grinding everything adds cost for no benefit. Specify which welds are cosmetic and which are structural, and let the rest be cleaned and coated.
What to confirm before production
- Which dimensions are critical: squareness, caster coplanarity, hole position, or assembled fit.
- Whether the order will repeat, and therefore whether a fixture should be built.
- Which welds are cosmetic and what finishing they require.
- Inspection points and whether a first-article trial assembly is required.
- Whether a prototype is needed before the production run.
Straight frames are the result of planning, not luck. Send your drawing and expected quantities, or see the quality control page for how we inspect before coating and dispatch.
Related pages: welding process, cage trolley, and workshop applications.
Have a Similar Trolley Project? Send It for Review
Send your trolley type, load capacity, size, wheel requirement, quantity, and drawings or reference photos. Our team will review the structure and reply within 24 hours on business days.
Urgent project? Email gao@doingmetal.com or WhatsApp +86 18158549983.